The industrial landscape is constantly evolving, demanding materials that can withstand extreme conditions while optimizing operational efficiency. Among these essential materials, the specialized application of stainless steel hardware cloth in the form of honeycomb conveyor belts has emerged as a pivotal solution for heavy-duty filtration and transport. By combining structural rigidity with an open-weave design, these components ensure that industrial processes remain seamless and durable.
Across various sectors, from food processing to chemical manufacturing, the need for a flat carrying surface that doesn't compromise on airflow or drainage is critical. Traditional belts often fail under high stress or succumb to corrosion, leading to costly downtime. This is where high-performance mesh solutions step in, providing a high strength-to-weight ratio that directly translates into lower energy consumption and increased equipment longevity.
Understanding the technical nuances of stainless steel hardware cloth and its integration into conveyor systems allows engineers to design more sustainable and efficient production lines. By prioritizing materials that offer both durability and a high open area, industries can achieve a superior balance between product throughput and system stability.
The Engineering Logic of Honeycomb Mesh
The honeycomb design is an engineering masterpiece tailored for applications requiring an open belt architecture without sacrificing a flat carrying surface. Unlike traditional weaves, the honeycomb structure provides an exceptional strength-to-weight ratio, which is essential for reducing the mechanical load on conveyor motors. This efficiency makes it an ideal choice for enterprises looking to lower their carbon footprint through reduced energy consumption.
Furthermore, the inherent stability of this design ensures positive drive and excellent belt tracking. By utilizing a structure reminiscent of high-grade stainless steel hardware cloth, these belts avoid the common pitfalls of sagging or drifting, which are frequent causes of product misalignment and mechanical wear in industrial conveyor systems.
Global Industrial Relevance and Standards
On a global scale, the demand for precision-engineered mesh is driven by the stringent requirements of ISO and other international quality standards. In industries where hygiene and corrosion resistance are non-negotiable, the transition toward high-grade stainless steel components has become the gold standard. The ability of these materials to withstand harsh chemical environments while maintaining structural integrity is a key factor in their widespread adoption.
Many manufacturers face the challenge of balancing open-area flow with load-bearing capacity. A belt that is too open may fail under weight, while one that is too dense inhibits drainage and airflow. The development of honeycomb-structured belts addresses this conflict, offering up to 81% open area, which facilitates an excellent flow-through for liquids, gases, or small particulates.
As global supply chains move toward automation, the reliability of the conveyor system becomes the heartbeat of the factory. Utilizing a robust stainless steel hardware cloth base ensures that the equipment can run for longer cycles with fewer interruptions, directly impacting the bottom line of large-scale industrial operations.
Core Components of High-Strength Belts
The durability of a conveyor belt is determined by its edge construction and joining method. High-performance belts typically feature either a welded button edge or a clinched edge, both designed to reduce snagging or catching on conveyor protrusions. This attention to detail prevents premature belt failure and ensures a smooth transition between different stages of the production line.
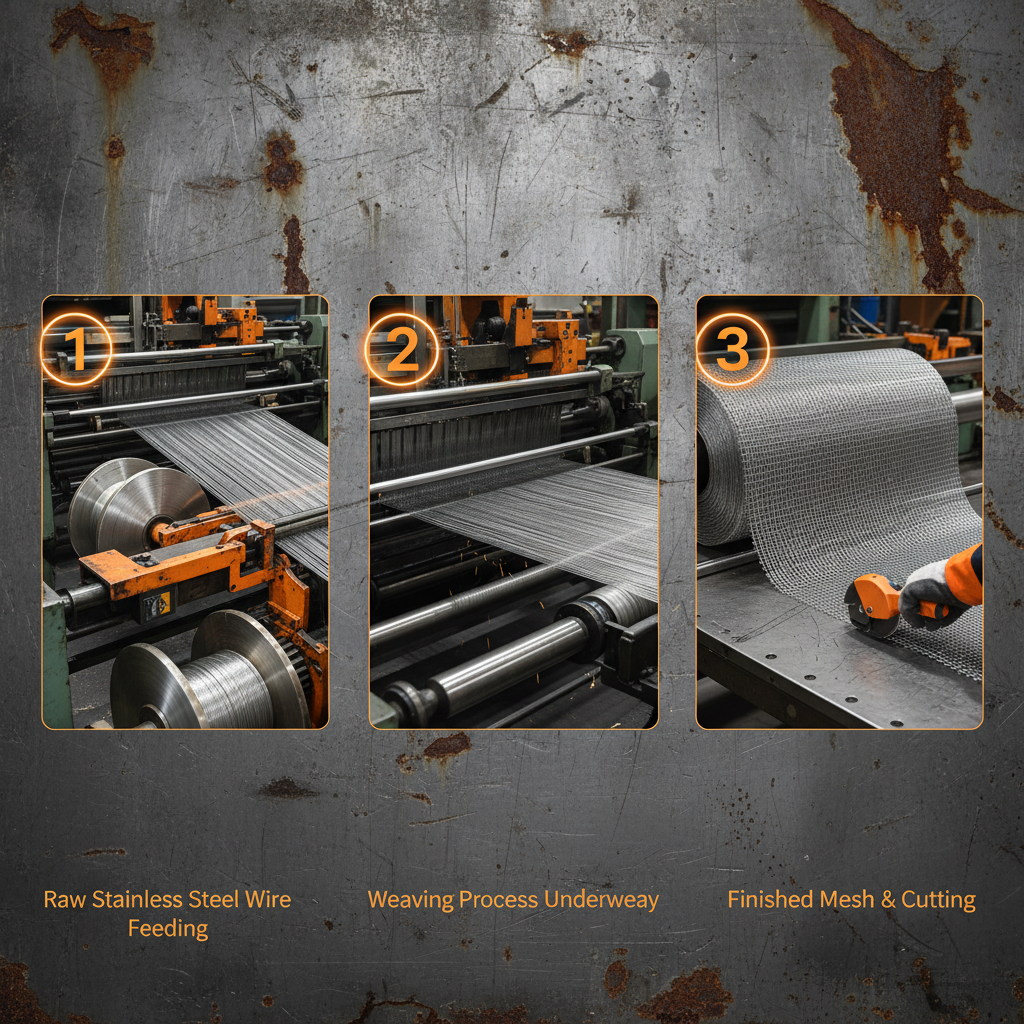
When comparing these systems to standard stainless steel hardware cloth, the honeycomb conveyor belt is engineered for twice the life of competitive belts. This longevity is achieved through superior material selection and a welding process that reinforces every intersection of the mesh, creating a rigid yet flexible surface.
Installation and maintenance are further streamlined by the fact that these belts require no special tools for setup. They are designed to be easily joined and cleaned, which is a critical requirement in food-grade environments where bacterial buildup must be prevented. This combination of ease-of-use and extreme durability defines the modern industrial standard.
Performance Metrics and Efficiency Gains
The operational efficiency of a conveyor system can be measured by its ability to handle tight transfers and maintain a flat surface under load. Honeycomb belts excel in these areas, allowing for precision movement of goods. Their high strength-to-weight ratio means that less torque is required from the motor to initiate movement, leading to measurable energy savings over thousands of operating hours.
To better understand the performance advantages, we can look at how different mesh configurations perform across key industrial KPIs. By optimizing the open area and the edge strength, manufacturers can significantly reduce the frequency of belt replacements and mechanical failures.
Comparative Performance of Mesh Configurations
Real-World Applications and Use Cases
In the food and beverage industry, the honeycomb belt is indispensable for frying and cooling processes. The high open area (up to 81%) allows oil to drain efficiently or air to circulate rapidly around the product, ensuring consistent quality. Because the surface is flat and made from high-grade stainless steel, it meets the strictest sanitary codes while resisting the corrosive effects of salt and acids.
Beyond food, these belts are utilized in remote industrial zones for mining and chemical processing. In these environments, the resistance provided by stainless steel hardware cloth technology is vital for transporting abrasive materials. The strong edges prevent the belt from snagging on protrusions, which is a common failure point in rugged industrial settings.
Long-Term Value and Sustainability
The long-term value of investing in honeycomb belts lies in the dramatic reduction of the total cost of ownership (TCO). With a lifespan that is twice that of competitive belts, the frequency of replacement parts and labor costs for installation is halved. This creates a logical financial advantage for plant managers who prioritize long-term stability over low initial procurement costs.
Sustainability is also a core benefit. The high strength-to-weight ratio reduces the energy required to move the belt, contributing to a lower overall electricity bill and a smaller carbon footprint for the facility. When combined with the recyclability of stainless steel, these belts represent a circular economy approach to industrial hardware.
Moreover, the reliability of the system fosters trust and safety in the workplace. Reduced belt failures mean fewer emergency repairs, which decreases the risk of industrial accidents associated with sudden machine stoppages. This emotional and logical peace of mind is an intangible but critical benefit for any operational team.
Future Innovations in Mesh Technology
The future of industrial mesh is leaning heavily toward digital integration and advanced material science. We are seeing the emergence of "smart belts" that can monitor tension and wear in real-time using embedded sensors. This transition from reactive to predictive maintenance will further extend the life of components based on stainless steel hardware cloth.
Automation and AI-driven design are also optimizing the honeycomb geometry. By using generative design, engineers can create mesh patterns that maximize airflow while further reducing weight, pushing the strength-to-weight ratio to new heights. These innovations ensure that the conveyor system can adapt to a wider range of product sizes and weights without requiring a full system overhaul.
As green energy becomes the global mandate, the focus will shift toward materials that require even less energy to manufacture and operate. The integration of specialized alloys that offer even higher corrosion resistance will allow these belts to operate in increasingly extreme environments, from deep-sea mining to aerospace component processing.
Core Specifications and Comparative Analysis of Honeycomb Belts
| Feature Dimension |
Honeycomb Specification |
Standard Mesh Performance |
Industrial Impact |
| Open Area Percentage |
Up to 81% |
40% - 60% |
Superior flow-through |
| Service Life |
2x Industry Avg |
Standard Baseline |
Reduced replacement cost |
| Max Width Capacity |
Up to 150 inches |
Up to 100 inches |
High-volume scalability |
| Edge Configuration |
Welded/Clinched |
Simple Folded |
Minimal snagging risk |
| Energy Efficiency |
High (Low Weight) |
Moderate |
Lower power consumption |
| Installation Effort |
No special tools |
Specialized tools req. |
Faster downtime recovery |
FAQS
Honeycomb belts are specifically engineered for transport, offering a flat carrying surface combined with a high open area (up to 81%). While general hardware cloth is excellent for screening, honeycomb belts provide a high strength-to-weight ratio and positive drive tracking, which are essential for preventing belt drift and reducing energy consumption in conveyor systems.
Depending on the application and environmental stressors, our honeycomb conveyor belts are designed to last twice as long as competitive belts. This is achieved through reinforced welded button edges or clinched edges that prevent snagging and a high-grade stainless steel composition that resists corrosion and mechanical wear.
No, one of the key advantages of this design is that installation requires no special tools. They are designed to be easily joined and installed, which significantly reduces the time and cost associated with initial setup or belt replacement during maintenance cycles.
Yes, they are ideal for food processing. The stainless steel material is naturally corrosion-resistant and hygienic, and the high open-area design allows for easy cleaning and efficient drainage of oils or water, ensuring that sanitary standards are maintained throughout the production process.
We provide high-capacity solutions available up to 150 inches wide. This allows industrial facilities to scale their production lines for larger products or higher volumes without compromising the stability or the flat carrying surface of the belt.
A higher strength-to-weight ratio means the belt is lighter without losing its load-bearing capacity. This reduces the inertia the motor must overcome to start and run the conveyor, leading to a decrease in kilowatt-hour consumption and overall energy costs over the life of the equipment.
Conclusion
The integration of honeycomb-structured stainless steel hardware cloth into conveyor systems represents a significant leap in industrial efficiency. By balancing a high open area with extreme durability and a flat carrying surface, these belts solve the age-old conflict between flow-through and structural stability. From reducing energy costs to doubling the service life of equipment, the tangible benefits make it a superior choice for any high-demand manufacturing environment.
Looking forward, the continued evolution of mesh technology will likely center on further weight reduction and the integration of smart monitoring systems. For enterprises aiming to optimize their production lines for sustainability and reliability, investing in precision-engineered stainless steel solutions is not just an upgrade—it is a strategic necessity. Visit our website for more information: www.stainlessmetalmesh.com